Vision Measuring Machine Factory: How Precision Measurement Systems Are Built
2026-10-19
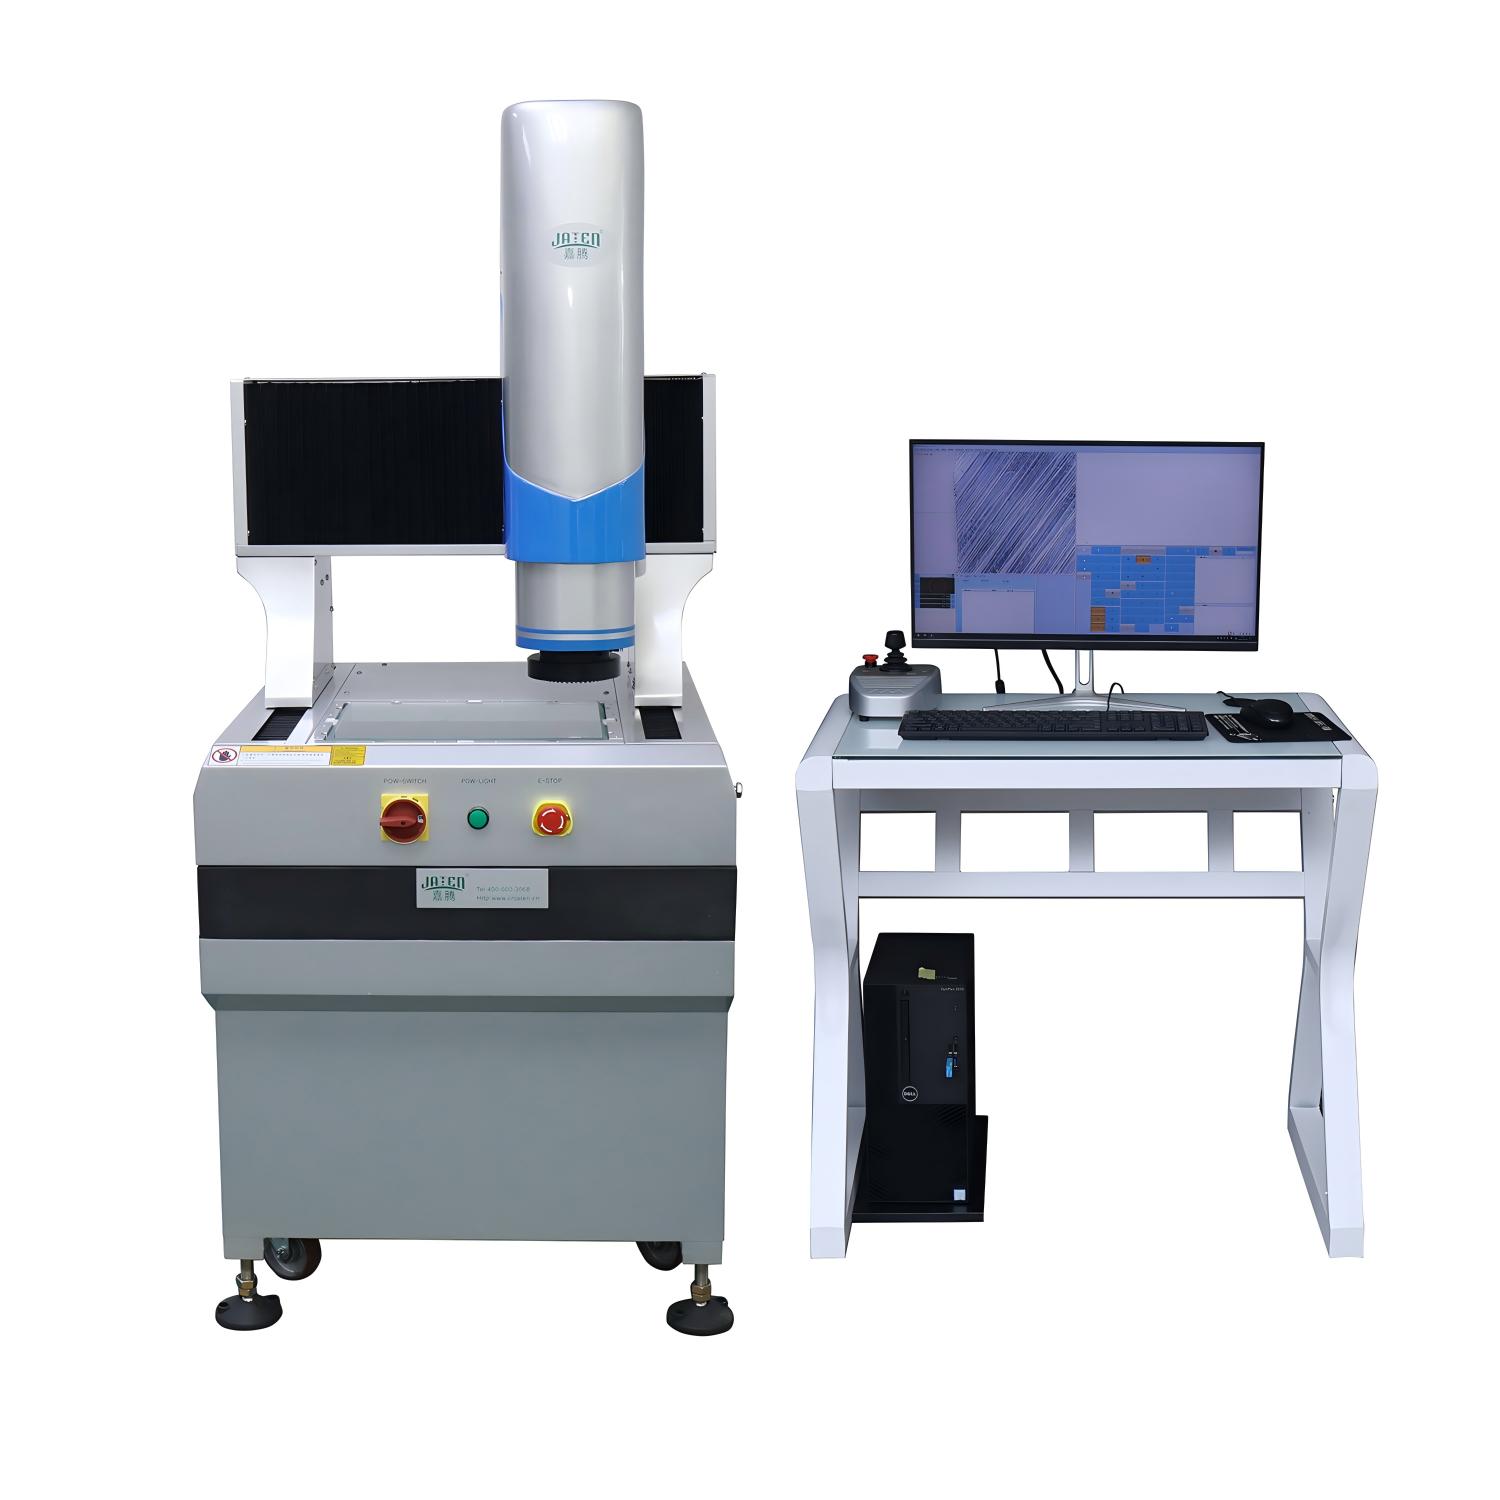
Peek inside a vision measuring machine factory and you won’t find assembly lines churning out generic parts. You’ll see temperature-controlled rooms, hand-scraped granite stages, and technicians aligning optics to tolerances measured in microns. That’s the reality at JATEN, where precision measurement systems are built through a blend of engineering discipline and relentless testing. Here’s a look at how those machines go from raw castings to the final accuracy certificate—and why every step matters.
Granite Before Anything Else
There is a reason granite still holds the top spot the moment you walk into a stone yard. Before tiles, before quartz slabs, before engineered mixes, your eye goes to the deep, unpredictable movement in a slab of real granite. It is not trying to be anything else. The veining does not repeat, the flecks of mica catch light differently from one corner to the next, and no two kitchens end up with the same story.
Granite before anything else also means making a decision about how you want a room to feel ten years from now. Painted surfaces wear, laminates peel, trends fade. Granite asks very little and gives back a kind of quiet permanence. You can set a hot pan down without flinching, slice on it with a little care, and still watch the polish hold through years of morning coffee and late dinners.
Most people expect granite to be the safe, traditional choice. Spend an afternoon looking at slabs, though, and that assumption falls apart. There are blues with storm-grey waves, blacks flecked with copper, greens that look pulled from a riverbed. Granite before anything else is not about settling. It is about choosing the one surface that does not have to imitate stone because it already is.
Hand Alignment, Then Laser Verification
The first pass is always by hand. You slide the bracket along the rail, feeling for the faintest catch or resistance. It's not about forcing it into place—it's about letting your fingertips read the surface. A few thousandths of an inch can hide in the texture, and once you learn to notice it, you stop trusting your eyes alone.
After the manual set, the laser comes in as a second opinion. Not to replace the hand work, but to catch what the skin can't. A rigid mount, a clean target, and the beam sweeping across the reference edge. The readout shows drift in real time. Sometimes the error is a fraction of a degree—enough to matter in a high-speed spindle or a linear stage.
The trick is not to rush between those two steps. Let the mechanical contact settle before the optics take over. If the laser disagrees with your alignment, walk back to the hand adjustment and make a small, deliberate change. Rinse and repeat. It's a slow loop, but the final numbers speak for themselves.
Cold Rooms and the Fight Against Thermal Drift
Maintaining a truly stable temperature inside a cold room is less about hitting a setpoint and more about managing the slow creep of thermal drift. Even when the refrigeration system cycles predictably, subtle changes in door seal compression, evaporator fan speed, or the thermal load from newly introduced items can push the air temperature a fraction of a degree off target over several hours. That small offset might seem harmless, but for sensitive equipment or stored samples it translates into measurable dimensional shifts and calibration errors.
The practical fight against drift often starts with reducing unnecessary air exchange. Strip curtains, fast-closing doors, and careful stacking to avoid blocking return air paths all help the control loop do its job without overcorrecting. Equally important is sensor placement: a probe mounted near the evaporator outlet will see a different world than one positioned where the actual work happens. Mapping temperature gradients under typical use conditions reveals hot and cold pockets that a single reading can easily miss.
Beyond passive measures, active strategies make a bigger difference. Some facilities use PID tuning that accounts for the thermal inertia of stored goods, while others add a small recirculation fan or a secondary trim heater to counteract overcooling during defrost cycles. Data loggers placed at multiple heights can catch drift before it becomes a problem, turning what used to be a reactive adjustment into a scheduled, evidence-based correction.
The Craft of Torque Sequences and Air Bearings
Torque sequences rarely get the attention they deserve. On a flange or a cylinder head, the order in which you pull each bolt to spec decides whether the mating faces sit true or quietly fight each other. A cross pattern isn't just tradition; it keeps the clamping force from walking across the part and pinching a high spot into a permanent warp. Many machinists will tell you the final pass feels different when the sequence is right—the wrench resistance climbs evenly, almost like the assembly is settling into itself.
Air bearings trade metal-to-metal contact for a thin film of compressed air, and that changes everything about how motion behaves. The gap might only be five microns, but it is enough to remove stiction and let a carriage glide with effectively zero static friction. The trick is keeping the supply clean and the load balanced. Too much pressure in one pocket and the bearing tilts; too little and it touches down, grinding away the very surface you were trying to protect. Working with them becomes a study in listening—hiss, drift, and the occasional back-pressure change all carry information.
Put torque sequences and air bearings side by side and the common thread is control of tiny, distributed forces. Neither rewards brute strength. One asks you to follow a pattern so the part never knows which bolt came first; the other asks you to maintain a boundary layer that is barely there. People who get good at both stop treating them as routine fastening or simple bushings and start treating them as systems with their own sense of balance.
Calibrating Against Artifacts with a Paper Trail
When precision matters more than assumption, calibrating against artifacts with a paper trail becomes the only defensible move. An artifact, in this sense, isn't junk — it's any enduring trace of a process, a decision, or an environment that refuses to be averaged away. The paper trail gives each artifact a story, a timestamp, a chain of custody. Without that trail, you're guessing at provenance; with it, you can weigh each data point by its context, not just its face value.
Think of a sensor that drifts over months, or a hand-edited logbook where ink smudges mark revisions. Calibration against raw averages fails because the artifacts carry hidden weights. A paper trail lets you separate the drift from the signal, the correction from the error. You're not cleaning the data so much as interrogating it — asking which artifacts deserve to anchor the calibration and which ones are red herrings wearing a timestamp.
In practice, this means building a ledger before you build a model. Every artifact gets a note: who touched it, when, under what conditions, and what was changed. Then calibration becomes a negotiation with the past, not a blind fit to the present. The result isn't a sanitized dataset; it's a defensible alignment where every adjustment can be justified by a line in the trail. That's the difference between precision and pretense.
Run-In Tests That Separate Microns from Promises
Initial run-in cycles do more than seat bearings or bed in gears—they act as a brutal audit of every tolerance claimed on a drawing. A spindle that passes static inspection at a micron of runout can reveal thermal drift, uneven preload loss, or micro-weld transfer within the first hour of loaded rotation. Those deviations rarely appear in catalog promises, but they show up plainly in vibration signatures and surface profilometry after break-in.
The gap between a spec sheet and a machine that holds size over a full shift often lives in the details nobody measures until parts start moving. Run-in tests force those details into the open: lubrication breakdown under shear, cage slip in high-speed bearings, or seal lips that polish themselves into leaks. By monitoring torque, temperature, and acoustic emission during controlled wear-in, engineers can separate harmless settling from defects that would later scrap a batch of parts.
What separates an honest tolerance from a hopeful one is repeatability under load, not a single-point check on a granite table. Run-in protocols that incrementally increase speed and load while recording displacement in real time expose the micron-level truths that matter for process capability. Promises stay on paper; run-in data walks onto the shop floor.
FAQ
The inbound area handles large granite blocks, aluminum extrusions, optical glass, servo motors, linear guides, and custom circuit boards. Each lot gets checked for dimensional conformity, surface finish, and electrical continuity before entering the clean assembly zone.
Granite arrives rough-cut and stress-relieved. The factory uses diamond grinding and lapping to bring the top surface within a few microns of flatness. Technicians then inspect it with autocollimators and electronic levels, and any high spots are hand-scraped until the entire working area meets the spec.
The bridge is mounted first, with its linear rails checked for parallelism using a laser interferometer. The camera and zoom lens are then attached to the Z-axis carriage. A calibration target with known dot spacing is placed on the granite, and the software adjusts pixel-to-micron ratios while the technician shims the lens mount until the optical axis stays perpendicular to the stage across the full travel.
Granite, steel, and glass expand at different rates. A shift of a couple degrees can change the distance between the scale and the read head enough to throw off a measurement by several microns. The room is held at 20°C ± 0.5°C, and components are left to soak for hours before critical alignments are touched.
The factory uses a laser interferometer as the reference standard. A moving carriage is driven in small increments along each axis while the interferometer records actual displacement. The machine's own readout is compared, and any nonlinearity is mapped into the controller's compensation table. This is repeated in both directions to account for backlash and hysteresis.
Most machining shops worry about low-frequency rumble from presses or forklifts. Here the concern shifts to high-frequency vibrations from HVAC blowers, nearby traffic, and even footfall. The granite base sits on passive air isolators with a natural frequency below 2 Hz, and some stations have active piezoelectric dampers that cancel residual vibration during the final accuracy tests.
The software is run through a scripted sequence using a known artifact: a glass plate with chrome circles at certified positions. The program measures each circle's diameter, roundness, and center-to-center distance, then compares the results to the calibration certificate. If any value deviates by more than the stated uncertainty, the error map is rebuilt or the optical setup is revisited.
After the initial calibration, the machine runs a stability test for 24 to 48 hours. It repeatedly measures the same feature and logs drift in X, Y, and Z. The factory also performs a thermal cycle by raising and lowering room temperature within a controlled range while checking that the compensation model keeps the readings stable. Only machines that pass both short-term repeatability and long-term drift limits get signed off.
Conclusion
Inside a vision measuring machine factory, precision starts long before any optics are mounted. Granite slabs arrive first, chosen for their stability and heft, then ground and lapped to a flatness that few machine shops ever see. From there, technicians perform hand alignment of critical axes, nudging components into place with feeler gauges and patience, before a laser interferometer sweeps the stage to confirm the geometry has held. Thermal control is not an afterthought; dedicated cold rooms keep assembly areas within a fraction of a degree, since even a stray breath of warm air can skew a measurement by several microns. The fight against drift is constant and almost meditative.
Torque sequences for bolts are followed like a recipe, with each fastener tightened in a specific order to avoid warping the structure, while air bearings float moving parts on a cushion of compressed air to eliminate friction and stick-slip. The machines are then calibrated against traceable artifacts—gauge blocks and step masters—with a paper trail that documents every adjustment and its uncertainty. Finally, each system endures run-in tests that run for days, cycling the stages repeatedly and comparing measurements to accepted standards. Only after these trials separate a reliable micron from a hopeful specification does the machine earn its place on the factory floor.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/