Vision Measuring Machine Supplier: Key Factors for Precision Manufacturing Success
2026-10-20
Every micron counts in precision manufacturing, and your measurement system is only as strong as the supplier behind it. Selecting a vision measuring machine supplier isn’t about ticking boxes—it’s about finding a partner who understands tolerance stacking, environmental drift, and the cost of a missed defect. Whether you’re automating in-line inspection or validating first articles, the right choice can mean the difference between seamless production and costly rework. This guide breaks down the factors that separate true metrology partners from equipment vendors, with insights drawn from companies like JATEN that treat measurement accuracy as a competitive advantage rather than an afterthought.
Precision Beyond the Datasheet
Most datasheets stop at nominal values and typical performance curves, but real precision shows up in the corners where numbers get soft. We test every unit across temperature swings, voltage droops, and load steps that never make it into the glossy PDF. The result is a part that behaves the same on your bench as it does on our worst-case simulation—no surprises when the enclosure heats up or the input rail sags.
Look closely at the fine print and you will find guard bands built around every spec, not just the headline accuracy figure. We characterize drift over time, not just at first power-up, and we publish the ugly percentiles alongside the median. If a parameter shifts under humidity or mechanical stress, we tell you before you design it in. That honesty is what turns a good datasheet into a trustworthy engineering document.
Precision beyond the datasheet also means our application engineers can hand you raw test data for the exact lot you are buying. No smoothing, no cherry-picked units. When your control loop depends on a few microvolts of offset or a handful of picoseconds of jitter, you will not find those answers in a typical product brief—but you will find them in our bench notes and silicon characterization reports.
Tailored Solutions for Complex Geometries
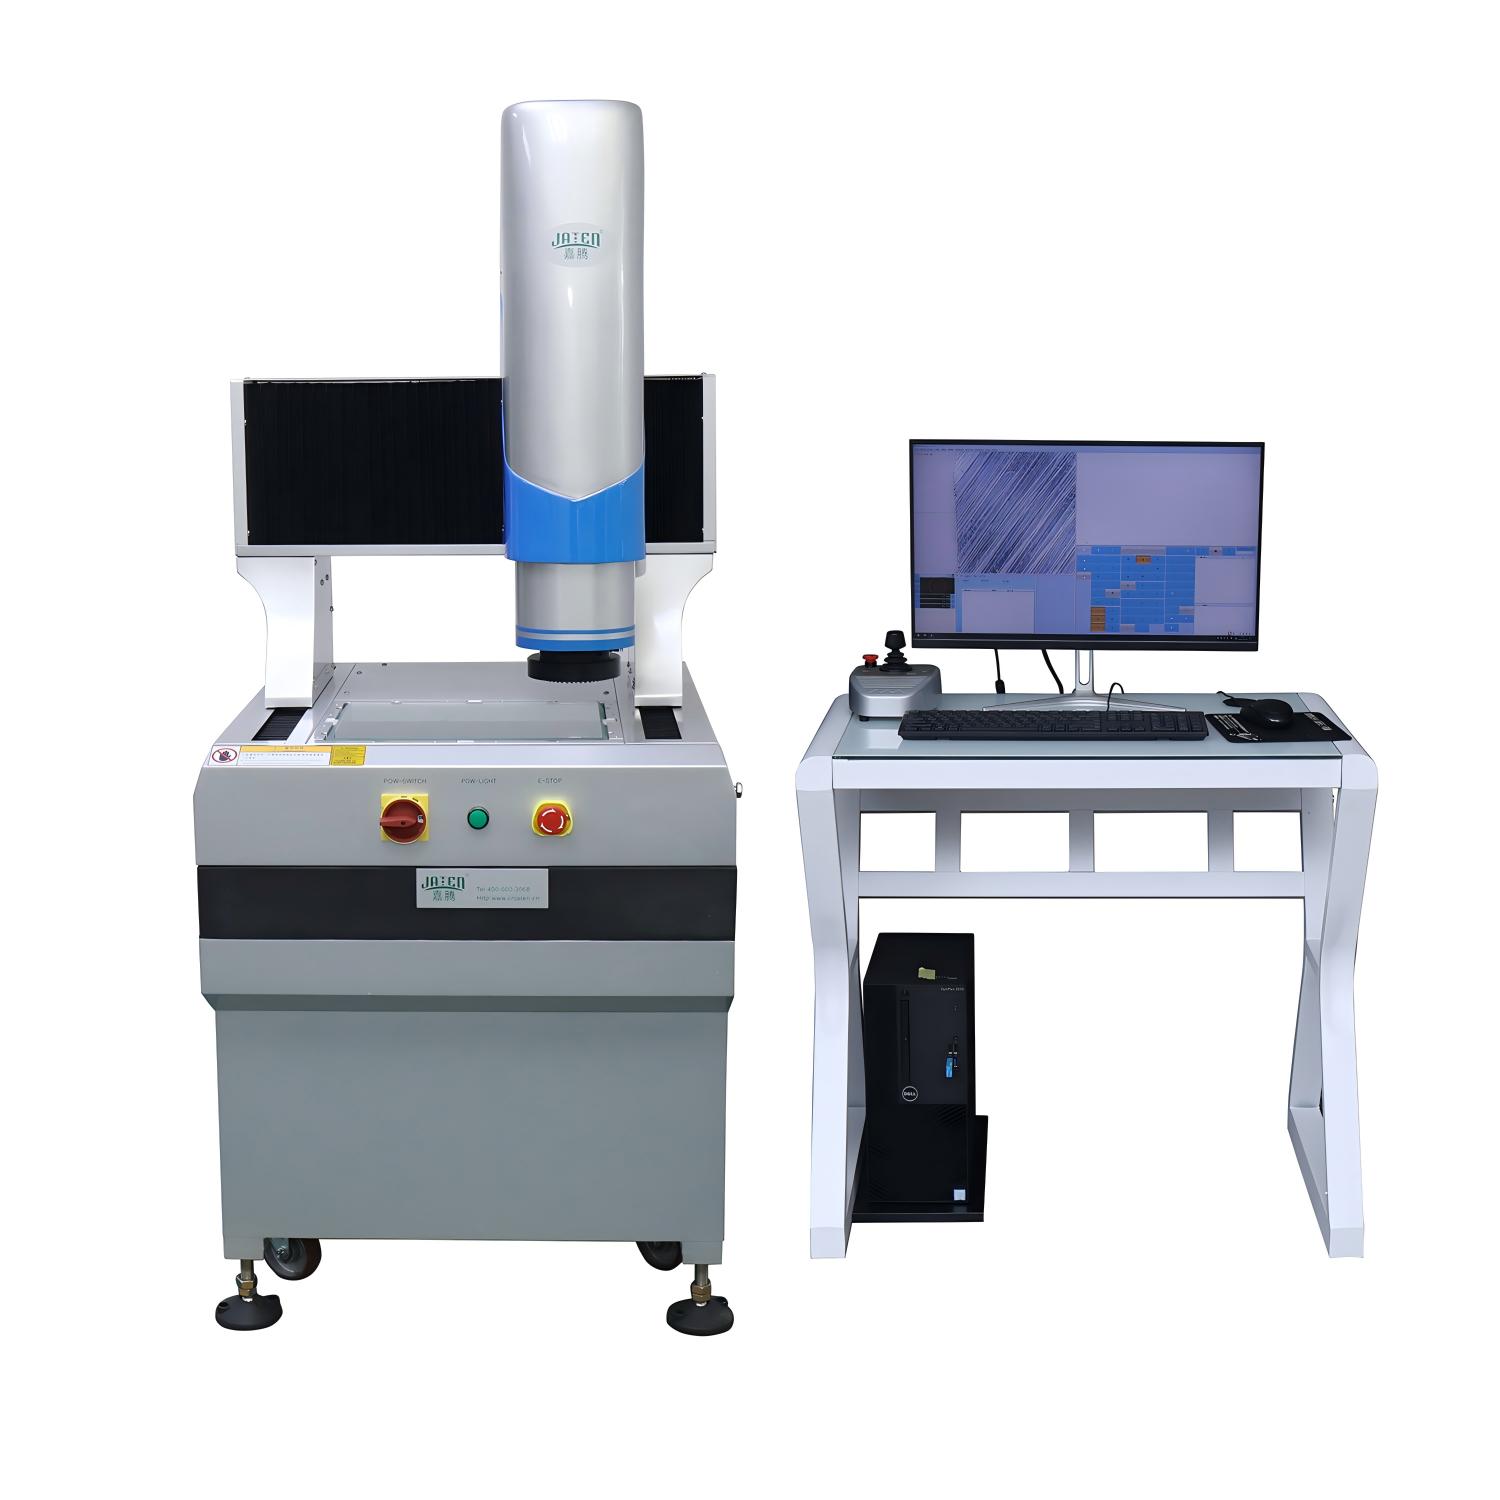
Every project brings its own set of dimensional puzzles—twisting channels, undercut cavities, or surfaces that refuse to follow a simple grid. Our approach starts by mapping the actual geometry, not forcing it into a pre-set template. That means we often build custom support structures, adjust tool paths mid-stream, and select materials that can handle tight radii without sacrificing strength.
We've tackled parts where standard fixtures simply couldn't hold the shape steady, so we designed low-profile clamping that followed the contour instead of fighting it. Other times, the challenge was internal: cooling passages that spiraled through a mold core. By working directly from the CAD model and prototyping in short loops, we turned what looked like a manufacturing headache into a repeatable process.
The result is a set of tailored solutions—not just a one-off fix. Whether you're dealing with thin walls, variable thickness, or joints that need to align across multiple planes, we adapt the method to the geometry, not the other way around.
Service Depth That Prevents Downtime
Instead of surface-level monitoring, this approach digs into the actual dependencies between systems. Every connection from a customer-facing API to a backend queue gets mapped and stress-tested, so a single slow query doesn't ripple into a full outage. Teams run failure drills during normal hours, not after an incident has already started.
Capacity planning is treated as an ongoing practice rather than a quarterly review. Traffic patterns are checked weekly, and scaling decisions are made before thresholds are reached. Critical data paths are duplicated and rehearsed, so failover isn't a theory—it's a routine that engineers know by heart.
When something does break, on-call staff aren't guessing. They have direct access to live runbooks, recent change logs, and incident timelines that show exactly where to look first. That depth of preparation keeps minor glitches from becoming customer-facing downtime.
Proven Track Record in Tight-Tolerance Industries
Tight tolerances separate shops that survive from those that just quote them. We've spent the last twelve years holding ±0.0001 inches on turned parts for implantable medical pumps and ±0.0004 inches on large aerospace housings. One long-standing client, a surgical robotics company, has rejected exactly zero of our 200,000 delivered components over the last four years—not because they're lenient, but because every batch arrives with full dimensional reports and statistically stable processes.
That kind of consistency doesn't come from luck. Our measurement lab runs CMMs, roundness testers, and laser micrometers that are calibrated every 90 days, and we perform GR&R studies before any new job goes to production. For a semiconductor equipment maker, we held a 4-micron linear tolerance across a 300-part lot of ceramic feedthroughs, with a process capability index above 1.67 on every critical dimension—something we documented and delivered with the shipment.
What really proves the track record is repeat business. Several of our tight-tolerance customers have been with us for more than a decade, moving new designs our way because they'd rather skip the supplier qualification cycle than risk a new vendor who hasn't earned that trust. When your parts can't be off by a hair, the strongest credential is a history of not being off at all.
Software That Simplifies, Not Complicates
Real simplicity isn't about stripping features into oblivion. It's about making the complex feel effortless, so the tool gets out of your way and lets you focus on the work itself. When software truly simplifies, you stop noticing the interface and start noticing the results.
The best tools aren't the ones with the longest feature lists—they're the ones that quietly handle the heavy lifting behind a clean, intuitive surface. You shouldn't need a manual to send a message or manage a project. If a core task takes more than a few seconds to understand, the software has already failed at its most important job.
Simplification also means respecting your time and attention. No buried settings, no distracting pop-ups, no forced workflows. Just the right amount of structure to keep you organized, and the flexibility to adapt without turning every action into a choose-your-own-adventure puzzle. That's the kind of simplicity people actually stay for.
Building a Partnership, Not Just a Purchase
Many suppliers treat a sale as the finish line, but real value appears later. When you build a partnership, your growth targets, production constraints, and customer feedback become part of the conversation. That means asking hard questions about lead times and material sourcing before they turn into emergencies.
A partnership also means you get honest recommendations, not just a catalogue. Sometimes the right answer is a lower-cost material that still meets your durability needs, or a phased rollout instead of a massive first order. That kind of counsel only happens when both sides have a stake in the outcome.
Over time, this relationship changes how problems are handled. A partner who knows your order history can spot a quality drift early, adjust packaging without being asked, and keep you updated before you need to chase status. The purchase is only the first step; the partnership is what keeps the product moving.
FAQ
The supplier's track record with parts similar to yours matters more than a glossy brochure. Ask for measured results on real components, not just spec-sheet numbers, and check how they handle thermal drift, vibration, and shop-floor lighting.
Software often decides whether operators trust the machine. Look for an interface that your team can learn in days, not months, and confirm that it can export data to your existing quality systems without extra add-ons.
Only if the machine is built for it. Granite bases, passive vibration damping, and stable optics help more than marketing claims. Request a live demonstration with your own parts during the hottest and busiest part of the day.
Calibration is not a one-time event. Choose a supplier with local technicians, clear preventive maintenance schedules, and fast access to replacement parts, because even small drift can scrap good work or pass bad parts.
Measuring a stamped connector is different from measuring a turbine blade or a plastic housing. A supplier who understands your materials, tolerances, and inspection routines will suggest fixturing and lighting that save time from day one.
Start with standard models unless your part geometry truly demands custom fixturing or unusual travel. Custom builds can lock you into a niche, while a proven standard platform usually has better resale value and faster spare parts.
Beyond the invoice, count in training days, software licenses, annual calibration, replacement illuminators, and the cost of tying up an operator during setup. A cheaper machine can become expensive if support calls drag on for weeks.
Conclusion
Selecting a vision measuring machine supplier involves far more than comparing datasheets. The best partners prove that their equipment holds accuracy not just in a calibration lab but on a busy production floor, where temperature shifts, vibration, and operator variability are real. They don't force your parts to fit a standard measuring envelope; instead, they configure sensors, staging, and lighting around complex geometries like deep bores, thin walls, or freeform surfaces. When a machine goes down, the cost isn't just repair time—it's stopped lines and missed shipments. That's why service depth matters: onsite spare parts, remote diagnostics, and technicians who understand your specific application can turn a potential week-long outage into a same-day fix.
A track record in tight-tolerance industries such as aerospace, medical devices, or precision tooling tells you the supplier has already weathered the demands of micron-level repeatability and rigorous documentation. But the software side often gets overlooked. The right platform guides operators through measurement routines without burying them in menus, making it easier to train new staff and reduce human error. Ultimately, the strongest suppliers act less like vendors and more like engineering partners—helping you refine inspection strategies, adapt to new product introductions, and scale quality control as your volumes grow. That kind of relationship pays off long after the purchase order is signed.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/