Walking Beam Quenching and Tempering Production Line for Oil Well Pipes Improves Strength and Extends Service Life
2026-11-18
Every ton of steel that goes downhole carries a simple promise: it has to hold. For oil well pipes, that promise is tested by pressure, corrosion, and fatigue long before anyone sees the failure. The walking beam quenching and tempering line changes the equation—uniform heating, controlled cooling, and a finer martensitic structure that turns standard pipe into a longer-lasting asset. At THINKING-LONG, we treat heat treatment not as a cost checkpoint but as a performance multiplier. Here’s why this production line is becoming the quiet advantage behind stronger, more service-ready oil country tubular goods.
Why Oil Well Pipes Fail Early and How Walking Beam Treatment Prevents It
Most early failures in oil well tubing are not the result of a single weak point. They happen because corrosion, cyclic loading, and mechanical wear reinforce each other in a confined space. Small pits caused by CO2, H2S, or sulfate-reducing bacteria create stress risers, and the repeated load swings from the pumping unit turn those pits into fatigue cracks long before the wall thickness is lost.
Rod and tubing contact adds another layer of damage. In deviated sections, the coupling scrapes the inner wall, removes protective films, and exposes fresh steel to produced water and oxygen. Once a wear groove forms, the local stress can rise sharply, and a crack may propagate from a groove that looks shallow at the surface.
Walking beam treatment shifts the focus from reacting to failures toward managing the load path and chemical environment together. By smoothing the reversal of the polished rod and adjusting stroke dynamics, it reduces the sharp acceleration spikes that drive fatigue. At the same time, batch or continuous treatment carried by the beam motion distributes inhibitor more evenly along the wear track, helping the film re-form where it is repeatedly scraped away.
Inside the Walking Beam Cycle That Builds Tougher Pipe Walls
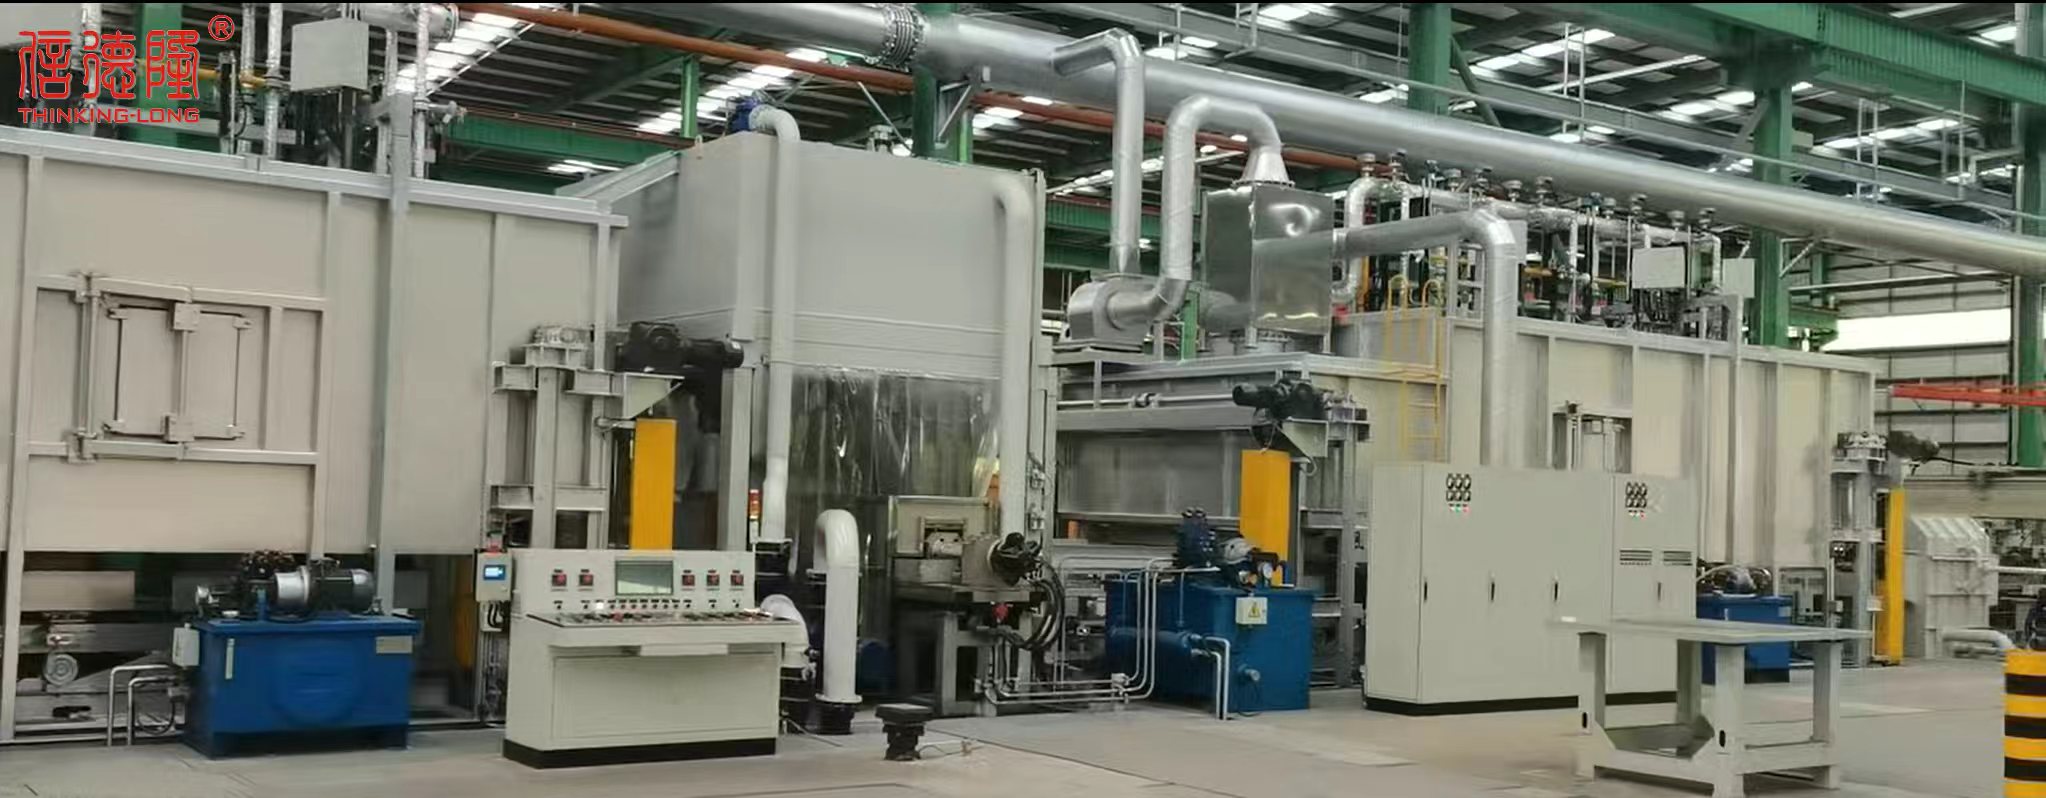
The walking beam cycle does more than shuttle pipe along the reheat furnace. Each forward stroke lifts the tube just enough to break surface contact with the skid, lets the furnace gas swirl underneath, and then sets it down in a slightly rotated position. That repeated lift-and-advance motion prevents the kind of dead zones that show up as soft bands in the wall, so the heat soaks inward from every side instead of pooling at the bottom.
What makes the cycle matter for toughness is the rhythm between movement and dwell. Operators tune the beam speed and pause time so the mid-wall reaches a narrow temperature band before the pipe rolls ahead. This controlled thermal path gives the steel enough time to dissolve coarse carbides without lingering so long that grains grow lazy. The result is a finer austenite structure before accelerated cooling, which carries over into a denser, more crack-resistant microstructure.
Small inconsistencies in the walking sequence show up later as uneven wall strength or residual stress spikes. A smooth cycle keeps the pipe advancing at a steady beat, allowing the wall to breathe evenly through transformation. That steadiness is what leaves the finished pipe with uniform hardness across the circumference and the kind of through-thickness toughness that holds up in cold climates and high-pressure service.
The Real Strength Story Behind Rapid Quench and Controlled Temper
Most people assume quenching is about raw speed, but the real story starts in the first few seconds when the surface and core stop agreeing on temperature. Rapid quench freezes a disorder that controlled tempering then negotiates into a usable structure. Hardness alone is a brittle claim; the temper gives the part enough flexibility to survive the real world.
Too aggressive a quench leaves cracks or distortion, too gentle a quench leaves potential untapped. Controlled temper is where those choices are settled. It removes only the stresses that cannot be trusted and keeps the ones that add fatigue life and dimensional stability.
What makes the result durable is not one dramatic step but the sequence. Rapid cooling creates the opportunity, and controlled reheating decides what that opportunity becomes. That relationship is the actual strength story behind the phrase, and it is earned in minutes rather than advertised on a data sheet.
How Uniform Heating Removes Hidden Weak Points Before They Reach the Field
Most hidden failures start with uneven heat. When one side of a part expands faster than the other, the material pulls against itself in ways that are easy to miss during inspection but show up later as cracks, warping, or premature wear. Those stresses get locked into the grain structure and travel with the component until the load and vibration of real operating conditions turn them into a fracture.
Uniform heating removes that gamble by bringing the entire cross-section up to temperature at the same rate. There is no steep thermal front pushing through the metal, so the grain transformation happens evenly and residual stress stays low. That also means hardness, ductility, and dimensional stability remain consistent from the surface down to the core, which is something spot heating or rushed cycles rarely achieve.
On a job site, the difference shows up in fewer unexplained early failures and less need for rework after installation. A part that was heated evenly tends to stay straight under load, hold its tolerances longer, and absorb shock without cracking along a hidden boundary. It is a quieter kind of reliability because nothing dramatic happens during production, but the weak points simply never get formed.
Extending Service Life Without Over-Alloying or Extra Weight
A common instinct in demanding environments is to reach for a richer alloy or add more mass, but that approach often trades cost and efficiency for marginal gains. Service life can instead be extended by tightening the variables that actually drive degradation: surface finish, residual stress, and local geometry. A smoother bearing journal, for instance, reduces the sites where pitting can nucleate, while controlled shot peening introduces compressive stress at the surface to slow crack growth. These adjustments require no extra material, yet they routinely push component life well beyond what a simple alloy upgrade would achieve.
Similarly, careful attention to lubrication pathways and load distribution can remove failure modes that heavier sections only mask. A redesigned fillet or a revised oil groove can lower peak contact pressure without increasing overall weight. In many cases, the difference between an early fatigue failure and a long, quiet service record lies in how the existing material is shaped and stressed. This approach treats the component as a system where geometry, finish, and operating conditions work together, rather than relying solely on chemistry to carry the burden.
The result is a longer operational window with no penalty in fuel consumption, rotational inertia, or raw material cost. Engineers who adopt this mindset often find that the same base steel or aluminum, processed and detailed correctly, outperforms a nominally stronger alternative that arrives with heavier sections and a higher price tag. Extending life becomes a matter of refinement rather than reinforcement, which keeps both the balance sheet and the vehicle mass in check.
What Well Integrity Data Reveals About This Heat Treatment Line
Well integrity data from the heat treatment line reads less like a routine quality log and more like a slow-burn diagnostic. Across several batches, the casing and coupling records show a pattern that isn't obvious on the surface: hardness values stay within spec, but the scatter in through-wall measurements widens in a predictable rhythm. That rhythm lines up with quench pressure dips, not with steel chemistry or incoming pipe dimensions. Once you see it, the data stops looking like noise and starts pointing at how the line actually behaves under load.
The more telling signal comes from the residual stress checks. Pipes that pass the standard acceptance window still carry a shallow tensile band near the mid-wall, something that only shows up when you overlay the data from different shifts. Day shift runs trend tighter, night shift runs drift toward the upper edge of the band. It isn't a defect in the traditional sense, but it's a signature of uneven cooling in the spray zone, and it repeats often enough that you can't blame operator error or a single batch of steel.
What this suggests is that the line's real bottleneck isn't throughput or temperature control in the furnace. It's the transition between the austenitizing soak and the quench start, where small timing differences get locked into the pipe wall as stress. If you were designing the next audit or deciding where to spend maintenance hours, the data makes a quiet argument: watch the transfer timing, the quench header pressure, and the rotation speed together. Those three variables explain more about long-term well integrity than any single hardness reading ever will.
FAQ
It hardens and tempers the pipes in a continuous, controlled pass so the final product can handle higher downhole pressures and resist fatigue over longer service intervals.
The beam motion lifts and advances each pipe without rolling or dragging, which keeps wall thickness uniform and reduces surface damage that could become a weak point later.
By producing a finer, more uniform martensitic structure through controlled quenching and tempering, the pipes become less prone to microcracking, corrosion fatigue and premature failure in aggressive well environments.
Depending on steel grade and pipe dimensions, yield strength can be raised to match API high-collapse or sour-service requirements while keeping elongation and toughness within usable limits.
Yes, it can accommodate a fairly wide range of oil country tubular goods by adjusting beam pitch, walking speed and quench intensity for each size so heating and cooling remain consistent.
The line uses zoned heating and rapid transfer into the quench, with sensors tracking each section; this prevents soft spots at the ends and avoids over-tempering in the middle.
Tempering relieves internal stress, converts brittle fresh martensite into a tougher condition and fine-tunes hardness so the pipe meets both strength and ductility requirements.
They are particularly useful in deep, high-pressure, sour gas or horizontal wells where collapse resistance, sulfide stress cracking resistance and long-term fatigue performance are critical.
Conclusion
Oil well pipes rarely fail because the steel lacks nominal strength on paper. They fail because local hard spots, uneven cooling after rolling, and residual stress create weak zones that crack under downhole loads, thermal cycling, and sour service. A walking beam quenching and tempering line addresses this by moving each pipe through a controlled sequence of heating, rapid quenching, and tempering without letting it rest in one position. The beam’s indexed motion keeps spacing consistent, so every joint receives the same thermal profile from end to end. Rapid quenching drives the wall into a martensitic structure, while the subsequent tempering step relaxes brittleness and locks in ductility. The result is a pipe wall that carries higher collapse and burst ratings while resisting the kind of early fatigue that shortens well life.
Uniform heating is the less visible part of the improvement. By bringing the entire pipe to an even austenitizing temperature before quench, the process removes hidden internal stress points that later become initiation sites for cracks. Field data from well integrity monitoring tells the same story: joints processed on this line show fewer pressure-related failures and slower corrosion-fatigue growth compared with conventionally treated pipe. That gain comes without adding extra alloy content or increasing wall thickness, which keeps weight and welding behavior practical. Over the full service window, the walking beam line shifts the failure curve outward, giving operators longer intervals between workovers and more predictable pressure containment.
Contact Us
Contact Person: Qian Xijun
Email: [email protected]
Tel/WhatsApp: 8613961736750
Website: https://www.thinkinglong.com/